
Industrial Grade Probiotic & Bulk Functional Ingredients
Our smart microbial fermentation plants run concurrently with high-purity active extraction units, manufacturing verified, COA-released raw materials calibrated for multinational supplement and food applications.
Ethyl Vanillin Powder High Quality Food Flavoring Agent
Source Material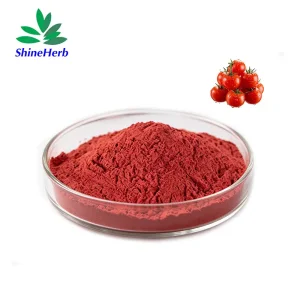
High-Quality Lycopene Powder for Male Wellness Supplements
Source Material
Food Grade Calcium Pantothenate Powder Vitamin B5
Source Material
Chenodeoxycholic Acid Powder CAS 74-25-9 High Purity
Source Material
High Purity Linolenic Acid ALA Raw Material
Source Material
Best Magnesium Glycinate Food Grade Chelate
Source Material
Kojic Acid Powder CAS 501-30-4 Skin Active
Source Material
100% Natural Phosphatidylserine Pure Soybean Extract
Source MaterialTaxonomy, Metabolism, & The Bio-Active Potency of Limosilactobacillus Reuteri
Formerly cataloged under the broad genus Lactobacillus, the phylogenetic reclassification to Limosilactobacillus reuteri highlights this species' unique co-evolutionary symbiosis with mammalian hosts, distinct carbon metabolic kinetics, and unmatched broad-spectrum antimicrobial production.
Reuterin (3-HPA) Biosynthesis
The definitive competitive advantage of L. reuteri is its capacity to metabolize glycerol via the glycerol dehydratase pathway into reuterin (3-hydroxypropionaldehyde). This potent, water-soluble antimicrobial agent inhibits both Gram-positive and Gram-negative pathogens including Helicobacter pylori, E. coli, Salmonella enterica, and Candida albicans without destroying natural commensal bifidobacteria.
De Novo Folate & Cobalamin Synthesis
Unlike homofermentative strains, selected genomic isolates of Limosilactobacillus reuteri possess complete operons for the bio-synthesis of functional vitamins, specifically Vitamin B12 (cobalamin) and dietary folates. This metabolic trait turns oral ingestion into an active, in-situ micronutrient delivery system inside the jejunum and ileum.
Epithelial Barrier & Tight Junction Fortification
Cell-wall associated surface-layer proteins (SlpA) and exopolysaccharides synthesized by L. reuteri directly interact with enterocyte TLR-2 receptors. This cascade activates up-regulated gene transcription for Occludin, Claudin-1, and ZO-1 tight junction proteins, actively suppressing gut hyperpermeability ("leaky gut syndrome") under cellular oxidative stress.
Why Global Brands Consolidate Probiotic Sourcing with Chinese Manufacturing
The convergence of vast automated fermentation capacities, indigenous upstream raw-material integration, and world-class microencapsulation tech positions Chinese bio-manufacturers as the dominant tier-one supply source for active probiotics globally.
50,000-Liter Deep-Tank Cascade Fermenters
Our Xi'an and regional manufacturing facilities utilize computer-controlled, fully enclosed multi-stage seed tanks cascading into automated 50-cubic-meter anaerobic fermenters. Continuous feedback loops monitor oxidation-reduction potential (ORP), real-time carbon consumption, and ammonia-feed neutralization to harvest cell densities exceeding $1.0 \times 10^{11}$ viable cells per milliliter.
Triple-Phase Cryoprotective Vitrification
The single greatest operational challenge with live anaerobic bacteria is cell lysis during lyophilization. Our industrial production applies a proprietary protective matrix of trehalose, sodium alginate, and pharmaceutical-grade skim milk solids that vitrifies the cell membrane without intracellular ice crystal rupture, ensuring unmatched live cell counts post-freeze drying.
Vertical Supply Chain & Cost Rationalization
By producing our own upstream peptones, carbohydrate feeds, and operating direct bulk milling, blenders, and packaging lines in Shaanxi's advanced biotech cluster, our clients gain direct primary-factory pricing. We eliminate trading tiers while offering complete cGMP, ISO, HACCP, Halal, and Kosher regulatory certification dossier packets.
Industrial Grade Limosilactobacillus Reuteri Specification
Every production batch undergoes full analytical profiling, combining microbiological quantification, heavy metal trace checks, flowability analysis, and thermal challenge assays.
| Analytical Parameter | USP / FCC Monograph Standard | ShineHerb Production Target | Testing Methodology |
|---|---|---|---|
| Viable Cell Count (CFU/g) | ≥1.0 × 10¹¹ CFU/g | 100B, 200B, or 500B CFU/g Customized | ISO/IDF 20128 / MRS Agar Flow Plate |
| Strain Identification | Conforms to L. reuteri | 16S rRNA Sequence & WGS Verified | PCR Gene Sequencing / MALDI-TOF MS |
| Moisture Content / Loss on Drying | ≤5.0% w/w | ≤3.5% w/w | Karl Fischer / Vacuum Desiccation |
| Water Activity (aw) | ≤0.20 | ≤0.12 (Strict moisture boundary) | Chilled Mirror Dew Point Instrument |
| Acid Resistance (pH 2.5, 2h) | ≥80% Survival | ≥92.5% Viable Retention | Simulated Gastric Fluid (SGF) Challenge |
| Bile Salt Tolerance (0.3% w/v) | ≥80% Survival | ≥90.0% Viable Retention | Oxgall Simulated Intestinal Fluid (SIF) |
| Heavy Metals (Pb, As, Cd, Hg) | ≤10.0 ppm combined | Pb<0.5ppm, As<0.5ppm, Cd<0.1ppm, Hg<0.1ppm | ICP-MS (Inductively Coupled Plasma) |
| Pathogenic Microorganisms | Negative / Absent | Absent in 25g (Salmonella, E. coli, Staph) | FDA BAM / Pharmacopoeia EP 2.6.13 |
Targeted Formulation Scenarios Across Global Sectors
Our engineering team works directly with formulation laboratories to match strain carriers, particle mesh sizes, and water activities to specific consumer packaging formats.
Pediatric Drops & Infant Colic
Clinically proven to shorten daily crying times in colicky infants by mitigating intestinal gas and neurogenic inflammation. Our specialized ultra-fine, oil-suspension grade powder disperses homogenously into medium-chain triglyceride (MCT) and sunflower oils without precipitation.
- Non-GMO sunflower lecithin carriers
- Zero rancidity degradation in liquid suspensions
Oral Healthcare & Periodontal Pastilles
L. reuteri competitively adheres to salivary pellicles, producing bacteriocins that suppress Streptococcus mutans and Porphyromonas gingivalis. Ideal for slow-dissolve mint lozenges, chewing gums, and probiotic effervescent mouthwashes.
- Direct-compression DC grade granular flow
- Maintains viable cell count under punching stress
Women's Urogenital & Barrier Formulations
Oral intake leads to secondary colonization of the vaginal epithelium, producing lactic acid to sustain a protective pH (≤4.5) while synthesizing hydrogen peroxide to block vaginal dysbiosis, bacterial vaginosis (BV), and recurrent candidiasis.
- Synergistic blending with D-Mannose & Cranberry
- High survival during mucosal barrier transit
Customized Formulation, Blending & Packaging Architecture
ShineHerb Biotech delivers complete contract manufacturing capabilities, taking bulk L. reuteri powder from primary fermentation into finished, consumer-ready retail delivery platforms.
Custom Carrier Customization
We tailor the inert substrate matrix based on our client's finished product claims. Options include Organic Maltodextrin, Prebiotic Inulin (FOS), Resistant Dextrin, Microcrystalline Cellulose (MCC), or Dairy-Free Isomalt for clean-label, vegan-certified dietary supplements.
Synbiotic Micro-Premixes
Bulk homogeneous dry blending under strict ISO Class 8 cleanrooms with dew points below -40°C. We formulate synergistic cocktails pairing L. reuteri with Bifidobacterium infantis, L. rhamnosus GG, zinc picolinate, bovine lactoferrin, and digestive enzymes.
Barrier Packaging & Cold Logistics
Probiotic viability demands complete atmospheric isolation. Our export shipments feature triple-layer heat-sealed aluminum foil barrier bags flushed with dry nitrogen (oxygen residual <0.5%), vacuum packing, desiccant liners, and optional data-logged temperature-controlled air freight.
Complementary Biochemicals, Enzymes & API Intermediates
In addition to custom probiotic blends, ShineHerb Biotech manufactures and exports verified pharmaceutical intermediates, vitamins, and specialized cosmetic actives for formulation procurement.
USP Fluorescein Sodium Salt CAS 518-47-8
Source Material
L-Carnitine Powder USP Standard API Material
Source Material
Wholesale 99% Trans-Pterostilbene CAS 537-42-8
Source Material
High Purity 98% Urolithin A CAS 1143-70-0
Source Material
Natural Chlorella Extract CGF Growth Powder
Source Material
Wholesale Vitamin K1 Phylloquinone Powder
Source Material
Food Grade Natamycin 50% Antifungal Powder
Source Material
Cosmetic Grade Syn-Ake Anti-Wrinkle Peptide
Source MaterialFrequently Asked Technical & Sourcing Questions
Answers to essential criteria vetted by quality assurance managers, contract packagers, and procurement directors evaluating wholesale Limosilactobacillus reuteri shipments.
Our standard commercial grades offer 100 Billion (1.0 × 10¹¹), 200 Billion (2.0 × 10¹¹), and ultra-concentrate 500 Billion CFU/g. Viability is enumerated utilizing ISO/IDF 20128 standard plate counts on MRS agar after 48-72 hours of strict anaerobic incubation at 37°C. Flow cytometry verification dossiers are available upon customer audit request.
Our factory uses a proprietary multi-layer microencapsulation matrix consisting of food-grade marine hydrocolloids and plant polysaccharides. This protective shell remains intact across the harsh acidic barrier of the stomach (pH 1.5–2.5), selectively dissolving upon encountering the neutral-to-alkaline pH and bile salts of the upper small intestine.
When stored in original sealed nitrogen-flushed foil packaging at -18°C or below, shelf life is validated for 24 months with less than 0.15 log loss. Under refrigerated conditions (4°C), stability is maintained for 18 months. With our microencapsulated grade, room temperature storage (25°C, dry environment) exhibits over 85% viability retention across 12 months.
Yes. Standard blends utilize pharmaceutical maltodextrin. For specialized clean-label requirements, we customize the carrier medium with organic inulin, resistant potato starch, soluble corn fiber, or rice flour. 100% dairy-free, allergen-free, vegan, and non-GMO formulation dossiers are available for all production lots.
Every batch ships with a dedicated Certificate of Analysis (COA) cross-referencing EP, USP, and FCC monographs. ShineHerb's manufacturing facilities are certified under cGMP, ISO 9001, ISO 22000, HACCP, Halal (MUI standard), and Kosher. Full technical data packages (TDS, MSDS, Allergen Statements, TSE/BSE declarations) are furnished during vendor audit qualification.
For commercial manufacturing partners, our standard production MOQ is 1 kg in heat-sealed aluminum pouches. We provide 50g–100g complimentary evaluation samples shipped via express air courier with dry ice or insulated cold packs for internal lab enumeration, compatibility screening, and dissolution trials.