
Featured Industrial Raw Materials & Synergistic Bioactive Compounds
Qualified bulk extracts, certified vitamins, and premium pharmaceutical precursors strictly manufactured under ISO/cGMP protocols for global formula developers.
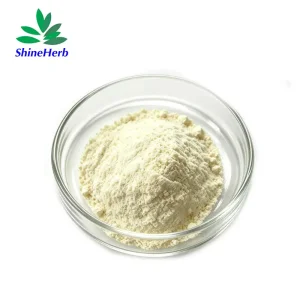
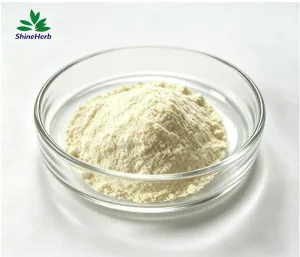
Industrial Engineering & Strategic Sourcing of Freeze Dried Honey Powder
An authoritative guide to vacuum sublimation thermodynamics, anti-caking glass transition (Tg) formulation, international botanical authentication, and supply chain risk mitigation.
Liquid honey has stood for millennia as humanity’s primary functional sweetener, revered for its antimicrobial, enzymatic, antioxidant, and humectant attributes. However, within 21st-century modern industrial manufacturing, raw liquid honey poses immense technical and operational hurdles. Its extraordinary hygroscopicity, high dynamic viscosity (ranging from 2,000 to 10,000 mPa·s at ambient room temperature), rapid crystallisation instability, and adherence to pneumatic bulk dosing equipment cause catastrophic downtime in automated production lines. Industrial buyers seeking to buy freeze dried honey powder wholesale do not merely seek a dried flavoring agent; they demand a crystalline, free-flowing, biologically active, shelf-stable, and chemically authentic powder suitable for dry blending, tableting, extrusion, and anhydrous cosmetic formulation.
This technical white paper establishes the baseline criteria for procurement officers, lead R&D scientists, and global supply chain directors evaluating international freeze dried honey powder wholesale suppliers and exporters. We investigate the molecular thermodynamics of apicultural freeze drying (lyophilization) versus legacy spray drying, examine carrier matrix stabilization architectures, present rigorous analytical authentication methodologies (EA-IRMS, LC-HRMS, and 1H-NMR), map localized high-yield industrial applications, and showcase the technological competitive moat realized through China’s advanced Smart Factory 4.0 manufacturing ecosystems.
1. Freeze Drying (Lyophilization) vs. Spray Drying: Molecular Thermodynamics
The global sweetener industry has witnessed a paradigm shift away from high-heat thermal dehydration. To appreciate why industrial purchasers increasingly insist on vacuum lyophilization, one must evaluate the structural carbohydrates comprising genuine bee honey. Raw honey typically contains 38.2% D-fructose, 31.3% D-glucose, 7.1% disaccharides (maltose, sucrose, isomaltose), and higher oligosaccharides, suspended with free amino acids, organic gluconic acid, and a suite of delicate bioactive enzymes including diastase (α- and β-amylase), invertase (α-glucosidase), glucose oxidase, and catalase.
In conventional spray drying, an atomized honey slurry is blasted with inlet air temperatures between 160°C and 195°C. Because the low-molecular-weight sugars (fructose and glucose) possess exceedingly low glass transition temperatures (Tg of fructose is approximately -42°C in aqueous solution and roughly 10°C to 16°C when fully dry), exposed monosaccharides immediately melt against drying chamber walls, forming a gummy, caramel-like resin. To overcome this sticky point during spray drying, manufacturers are forced to dilute honey with 50% to 70% low-cost corn maltodextrin or silica carriers. Furthermore, the extreme thermal exposure irreversibly denatures the enzymes, degrades phenolic flavonoids (such as pinocembrin, chrysin, and quercetin), and produces toxic condensation byproducts such as 5-hydroxymethylfurfural (5-HMF), which frequently exceeds European Union statutory safety thresholds (>40 mg/kg).
In contrast, industrial freeze drying (lyophilization) executes sublimation across three meticulously controlled phases governed by the thermodynamic triple point of water (0.01°C, 611.65 Pa):
- Phase 1: Deep Blast Cryogenic Freezing (-45°C to -50°C): The pre-homogenized liquid honey blend undergoes controlled flash freezing, forming microcrystalline ice matrices. This ultra-fast temperature plunge prevents large ice crystals from shearing the native apicultural protein structures and locks the aromatic terpene volatiles in place.
- Phase 2: Primary Sublimation under Ultra-High Vacuum (10 to 30 Pa): Under deep vacuum conditions inside industrial vacuum chambers, shelf temperatures are slowly modulated from -30°C to 0°C. Water molecules sublimate directly from solid ice crystals into gaseous vapor without passing through the liquid phase. Over 90% of unbound moisture is removed at ambient temperatures well below the denaturation threshold of invertase and glucose oxidase.
- Phase 3: Secondary Desorption Post-Drying: Residual bound water molecules residing within the carbohydrate matrix are extracted under elevated vacuum and strictly regulated shelf warmth (+20°C to +25°C). The resulting crystalline cake achieves an equilibrium water content of less than 2.5% and a water activity (Aw) below 0.20, effectively starving all microbial, osmophilic yeast, and mold proliferation vectors.
| Analytical Parameter | Industrial Freeze-Dried Honey Powder | Commercial Spray-Dried Honey Powder | Raw Unprocessed Liquid Honey |
|---|---|---|---|
| Operating Processing Temperature | -45°C to +25°C (Sublimation) | +160°C to +195°C (Flash Heat) | Ambient (Unheated) |
| Enzymatic Retention (Diastase / Invertase) | > 92% Native Retention | < 5% (Total Thermal Denaturation) | 100% Baseline |
| Volatile Aromatic Recovery (Terpenes/Esters) | > 95% Characteristic Aroma | < 15% (Burnt / Caramel Odor) | 100% Native Fragrance |
| Moisture Content & Water Activity (Aw) | Moisture < 2.5% | Aw < 0.20 | Moisture 4.0% - 6.0% | Aw ~0.35 | Moisture 17.0% - 20.0% | Aw ~0.60 |
| Honey Solids Content (Active Ratio) | 70% to 100% Pure Honey Options | Typically 30% to 50% Honey (Heavy Carriers) | 100% Honey Solids |
| Reconstitution Rate & Cold Solubility | < 15 seconds in cold water (>99.4%) | 45 - 90 seconds (Prone to lumps) | Slow dissolution in cold matrices |
| 5-Hydroxymethylfurfural (5-HMF) Formation | < 10 mg/kg (No Heat Production) | > 55 mg/kg (High Heat Reaction) | 5 to 20 mg/kg depending on age |
2. Carrier Matrix Optimization: Overcoming the Fructose Caking Phenomenon
A frequent failure mode encountered by procurement teams when importing freeze-dried honey from unsophisticated processors is rapid post-packing agglomeration—wherein a free-flowing powder solidifies into an unworkable, rock-hard block within days of container unpacking. This disaster stems from a failure to manage the Glass Transition Temperature (Tg) of amorphous monosaccharides.
Because pure honey fructose has a glass transition temperature of approximately 10°C to 16°C, exposure to warm ambient processing air (25°C) causes the powder to shift from its rigid, brittle "glassy" state into a viscous, rubbery "rubbery" state. At this point, liquid bridges form between neighboring particles, leading to irreversible solid caking. Professional freeze-dried honey manufacturers engineer the glass transition envelope using customized carrier technologies:
Option A: Non-GMO Clean-Label Tapioca & Chicory Inulin Fiber (Soluble Prebiotic Carrier): Designed for functional sports nutrition and clean-label dietary supplements. Replacing synthetic silica or corn-derived fillers with certified Non-GMO prebiotic fiber raises the overall composite glass transition temperature (Tg) above 55°C. This allows the finished powder to remain completely free-flowing even when shipped across humid tropical equatorial shipping corridors without requiring controversial synthetic anti-caking agents such as silicon dioxide (E551) or tricalcium phosphate.
Option B: 100% Pure Vacuum Sublimated Honey Micro-Crystals (Carrier-Free): Formulated specifically for anhydrous pharmaceutical applications, clinical infant nutrition premixes, and luxury cosmetic scrubs. Carrier-free freeze-dried honey powder requires hermetic cleanroom processing inside ISO Class 7 production suites with humidity continuously throttled below 20% RH. The powder is instantaneously vacuum-sealed or nitrogen-purged into multi-layer aluminum foil barriers directly on the discharge line to prevent atmospheric moisture pickup.
Option C: Organic Rice Flour / Acacia Gum (Certified Organic Matrices): Built strictly to satisfy USDA NOP and EU Organic (EC 834/2007) standards. Acacia gum (gum arabic) acts as an exceptional protective film-forming hydrocolloid, microencapsulating delicate honey volatiles while conferring resistance to mechanical shear stress during dry ribbon blending and tableting.
3. Global Procurement Demands: Authenticity, Zero Adulteration & Traceability
Global regulatory bodies and consumer watchdogs have placed the apiculture industry under unprecedented analytical scrutiny. Liquid honey is notoriously one of the top three most adulterated food commodities on earth, frequently diluted with industrial C4 corn syrups, C3 rice syrups, beet syrups, and inverted high-fructose syrups. When sourcing bulk freeze-dried honey powder wholesale, enterprise procurement departments face severe legal and reputational risks if testing is not embedded into every batch COA (Certificate of Analysis).
A tier-1 global freeze-dried honey exporter must provide batch-specific third-party laboratory verification (via world-renowned testing facilities such as Intertek, Eurofins, or QSI) adhering to the following pharmaceutical-grade testing standards:
- EA-IRMS (Elemental Analyzer - Isotope Ratio Mass Spectrometry): Quantifies the stable carbon isotopic ratio (δ13C) between the bulk honey carbohydrate fraction and the isolated honey protein fraction. A δ13C variance exceeding statutory thresholds confirms illicit adulteration with C4 photosynthetic plant sugars (corn syrup or cane sugar) according to AOAC Method 998.12.
- LC-HRMS & 1H-NMR Profiling: Employs high-resolution nuclear magnetic resonance spectroscopy and liquid chromatography-high resolution mass spectrometry to establish an unalterable metabolic fingerprint. This screens against sophisticated C3 exogenous syrups (such as rice syrup or beet syrup), verifies botanical origin, and confirms geographic authenticity down to specific apicultural floral ecosystems.
- Antibiotic & Veterinary Residue Screening: Zero tolerance testing for veterinary compounds via LC-MS/MS. Every export consignment is rigorously confirmed free from chloramphenicol, nitrofurans (AHD, AOZ, AMOZ, SEM), sulfonamides, fluoroquinolones, streptomycin, and tetracyclines with limits of detection throttled below 0.1 μg/kg (ppb), guaranteeing frictionless customs clearance into the European Union, the United States (FDA 21 CFR Part 117), Japan (MHLW Positive List System), and the Middle East.
- Pesticide & Neonicotinoid Panels: Comprehensive multi-residue pesticide screens covering over 500 agricultural chemicals, specifically ensuring glyphosate, imidacloprid, clothianidin, and thiamethoxam fall far below stringent EU Maximum Residue Limits (MRLs).
China Factory 4.0: Supply Chain Resilience & Processing Supremacy
How Shaanxi’s high-tech industrial bio-manufacturing corridor delivers uncompromised sublimation volume, automated cleanroom safety, and rapid multimodal international dispatch.
Continuous Lyophilization Tunnels
Equipped with automated continuous freeze-drying tunnel systems spanning over 8,600 m² of specialized GMP bio-processing space. Real-time computerized sublimation controllers ensure uniform vacuum pressure and cryogenic temperature profiles across every tray, eliminating lot-to-lot moisture variance.
Qinling Mountain Apiculture Corridors
Directly integrated with certified apiaries located within the pristine Qinling Mountain ecosystem. With raw acacia, polyfloral, and jujube honey sourced from isolated high-altitude reserves free from industrial runoff, our botanical purity and native enzyme counts consistently lead global industry benchmarks.
Automated Cleanroom Packaging
Milling, sifting, and bulk packaging take place inside fully automated ISO Class 7 cleanrooms with HEPA-filtered positive pressure air and relative humidity held below 20%. Triple-laminated nitrogen-flushed EVOH/foil barrier bags permanently lock out oxygen and atmospheric water vapor.
Digital Batch Traceability
Every export carton is linked to a QR-coded digital traceability register recording harvest date, apiary registration number, raw moisture level, vacuum sublimation logs, milling mesh size, and full analytical chromatography panels. Complete audit-ready documentation provided in under 12 hours.
Multimodal Silk Road Freight Hub
Situated in the Xi'an Hi-Tech Zone, our supply chain directly leverages Xi'an International Port’s direct railway express to Europe (12-14 days transit) and rapid customs-cleared air freight lanes to North America, Southeast Asia, and Dubai, lowering international freight overhead by up to 28%.
Localized Application Scenarios & High-Yield Formulations
Discover how global formulators across nutraceuticals, functional beverages, gourmet bakery, and cosmeceuticals deploy freeze-dried honey powder to resolve production bottlenecks.
Nutraceutical Sachets & Drink Mixes
Instantaneous cold-water reconstitution allows formulators to integrate real, enzymatic honey powder into immune-boosting drink mixes, collagen peptide blends, electrolyte hydrators, and herbal wellness teas without sediment clumping or foaming.
Engineered particle mesh sizes (60 to 120 mesh) confer excellent flowability, compactibility, and compressibility in rotary tablet presses. Imparts natural honey sweetness, masking bitter active botanicals such as Curcumin, Berberine, or B-Complex vitamins.
Eliminates the sticky mess of liquid honey injection on industrial bakery lines. Delivers consistent caramelization, golden crust coloration, and natural humectancy to artisan crackers, gluten-free cookies, granola clusters, and dry meat rubs.
Because water drives bacterial contamination in clean cosmetics, carrier-free freeze-dried honey powder is ideal for anhydrous powder facial cleansers, enzymatic exfoliating scrubs, and micro-peel masks, delivering intact natural gluconic acid and antioxidant polyphenols.
Provides authentic honey labeling ("Contains Real Honey") without disturbing the precise critical water activity and gelling temperature of automated starch mogul depositors, preventing gummy weeping and mold formation.
Frequently Asked Questions (FAQ) for Importers & Formulators
Expert answers addressing regulatory clearance, minimum order volumes, bulk packaging barriers, stability data, and custom carrier customization.
What is the minimum shelf-life of bulk freeze-dried honey powder and what are the recommended storage protocols?
Can your factory supply 100% pure carrier-free freeze-dried honey powder without maltodextrin or additives?
What regulatory and safety documentation accompanies each export consignment?
How does freeze-dried honey powder perform in terms of dissolution speed and clarity in liquid beverage formulations?
What is your factory’s standard bulk export packaging format to protect against transit humidity?
What is the typical Minimum Order Quantity (MOQ) and production lead time for international B2B orders?
Explore Additional Pharmaceutical & Dietary Actives
Expand your brand's master formulation pipeline with high-purity cosmeceutical precursors, specialized joint repair compounds, and stabilized liposomal delivery powders.
Accelerate Your Commercial Formulation with Certified Raw Materials
Connect directly with our senior application chemical engineers and export documentation officers in Xi'an. Receive complete analytical dossiers, third-party EA-IRMS testing certificates, custom mesh samples, and CIF/FOB wholesale pricing within 24 business hours.
Request Technical Dossier & Commercial Quotation